VertexFlow Tubes stainless steel tube manufacturer logo VertexFlow TubesPrecision SS Tubing

Wholesale Muffler Core Tube Manufacturers & Factory

High-Gain Acoustic Engineering, Micro-Perforation Metallurgy & High-Temperature Exhaust Tubing Solutions for OEM & Global Tier-1 Aftermarket Supply Chains

Precision Tubing Catalog Part I

Industrial & Structural Stainless Steel Tubing

Explore our precision-engineered stainless steel tubing solutions, manufactured under strict ISO 9001 and IATF 16949 quality control protocols.
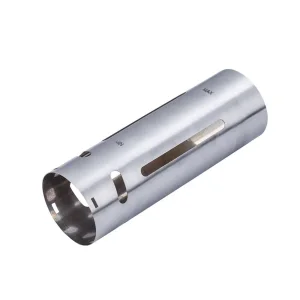
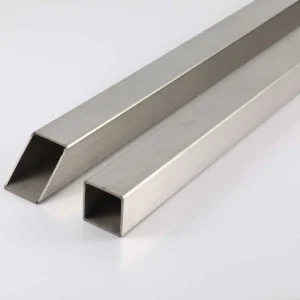
China OEM Stainless Steel Tube Fabrication & CNC Machining Manufacturers, Suppliers

China OEM Stainless Steel Tube Fabrication & CNC Machining Manufacturers, Suppliers

View Details
High-Quality Medical Grade Stainless Steel Tubing for Hospital Furniture Factories, Factory

High-Quality Medical Grade Stainless Steel Tubing for Hospital Furniture Factories, Factory

View Details
China Decorative Stainless Steel Tubing for Furniture (201 & 304) Manufacturer, Supplier

China Decorative Stainless Steel Tubing for Furniture (201 & 304) Manufacturer, Supplier

View Details
ODM Marine Grade 316L Stainless Steel Tubing Manufacturer, Suppliers

ODM Marine Grade 316L Stainless Steel Tubing Manufacturer, Suppliers

View Details
OEM Stainless Steel Tubing for Industrial Racks & Workstations Manufacturer, Factories

OEM Stainless Steel Tubing for Industrial Racks & Workstations Manufacturer, Factories

View Details
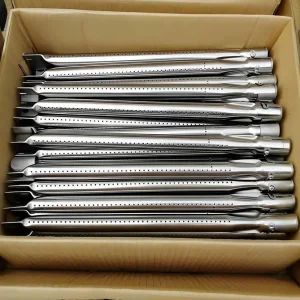
OEM Stainless Steel Gas Grill Burner Tubes (OEM & Aftermarket) Supplier, Factory

OEM Stainless Steel Gas Grill Burner Tubes (OEM & Aftermarket) Supplier, Factory

View Details
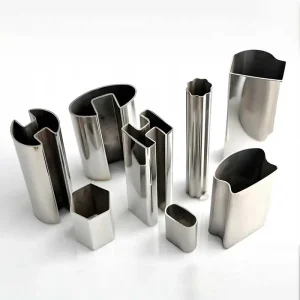
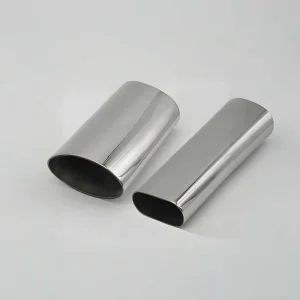
OEM ASTM A554 Stainless Steel Oval & Special Shaped Tubing Manufacturers, Supplier

OEM ASTM A554 Stainless Steel Oval & Special Shaped Tubing Manufacturers, Supplier

View Details
High-Quality Stainless Steel Tubing for Home Storage & Organization Manufacturers, Supplier

High-Quality Stainless Steel Tubing for Home Storage & Organization Manufacturers, Supplier

View Details
Industry White Paper & Technical Insights

The Metallurgical & Acoustic Architecture of Modern Muffler Core Tubes

In modern automotive exhaust system design, the muffler core tube—often referred to as the perforated inner pipe or acoustic core—serves as the primary structural and acoustic element inside silencers, resonators, and catalytic converters. Operating within an extremely hostile working environment characterized by thermal shock (ranging from ambient temperatures to over 850°C), aggressive chemical condensate (nitric, sulfuric, and organic acids), and intense gas pulsation, the muffler core tube must balance structural integrity with optimal noise attenuation and backpressure optimization.

Core Information Gain: Advanced muffler core manufacturing requires balancing perforation porosity ratios (typically 18% to 38%) against structural wall collapse limits under high-cycle fatigue, while selecting precise alloy chemistries (such as 409L ferritic stainless steel or 304 austenitic steel) to prevent oxidation scaling and intergranular stress corrosion cracking.

Acoustic Attenuation Physics

Perforated core tubes operate as Helmholtz resonators and dissipative silencer elements. The size, pitch, and distribution of perforated holes govern the acoustic impedance of the exhaust path. By tuning the open area ratio (OAR), acoustic energy from engine firing frequencies is converted into thermal friction as gas pulses pass through the perforation matrix into sound-absorbing packing fibers (such as basalt wool or E-glass fiber mats).

High-Speed Perforation Engineering

Modern manufacturing demands burr-free punch perforation or high-speed louvering. Intruding burrs inside the tube create undesired flow turbulence and high-frequency whistling, while rough external burrs shred fiberglass packing during muffler assembly. VertexFlow utilizes CNC rotary punch presses maintaining punch-to-die clearances within 0.02 mm.

Thermal Expansion & Fatigue Resistance

Exhaust temperatures vary drastically between short urban trips and sustained highway driving. Ferritic stainless steels like 409L and 439 possess lower thermal expansion coefficients compared to austenitic 304, minimizing stress concentration at end-cap weld joints and preventing premature acoustic core buckling.

43+
High-Precision Tube Mills
12,000m²
Specialized Production Facility
±0.03mm
Dimensional Outer Tolerance
500+
Existing Perforation Dies & Tooling
Macro Market Solutions

Global Enterprise Procurement Trends in Automotive Muffler Components

The global automotive exhaust system market is undergoing significant technological restructuring. Tier-1 automotive suppliers, aftermarket exhaust system manufacturers, and heavy-duty equipment OEMs are adjusting their procurement criteria based on evolving regulatory standards, environmental policies, and vehicle architecture shifts.

1. Hybrid Electric Vehicle (HEV & PHEV) Exhaust Dynamics

Hybrid powertrains introduce unique challenges to exhaust systems. Frequent internal combustion engine (ICE) cycling causes the muffler core to remain below the dew point for longer periods, resulting in severe acid condensate accumulation. Global buyers increasingly mandate 439 or 304L stainless steel cores with anti-corrosion passivation coatings to withstand cold-start acid attacks.

  • High resistance to acidic dew-point condensation.
  • Superior low-frequency sound dampening for engine re-ignition transients.
  • Extended warranty compliance (up to 10 years / 150,000 miles).

2. Stringent Acoustic & Emissions Regulations (Euro 6d / Euro 7 & US EPA Tier 4)

Noise pollution regulations across Europe, North America, and Asia have tightened decibel limits for drive-by sound testing. Muffler cores must maintain precise perforation pitch and zero hole deformation during bending or expand-end processing. Custom louvered tubes are rapidly replacing standard round holes to disrupt standing waves without increasing exhaust backpressure.

  • Helical and direct-louver geometries for optimized acoustic wave scattering.
  • Zero-burr internal surfaces reducing backpressure by up to 12%.
  • Strict compliance with ISO 362 drive-by noise test standards.

3. Supply Chain Rationalization & Near-Net Material Efficiency

Procurement directors are shifting away from buying standard mill-length tubes that require secondary cutting, deburring, and slotting at local assembly plants. Wholesale buyers now demand pre-cut, pre-end-formed (flared, expanded, slotted, or notched) muffler core components delivered direct-to-line, eliminating scrap rates and secondary labor costs.

  • JIT (Just-In-Time) component delivery kits.
  • Integrated secondary CNC end-forming (swaging, expand-fit, and slotting).
  • 100% automated optical inspection (AOI) per batch.

4. Lightweighting via Thin-Wall High-Strength Stainless Alloys

To meet fleet fuel economy targets, OEMs are reducing muffler wall thickness from traditional 1.5mm to 0.8mm–1.0mm. Achieving structural rigidity in thin-wall perforated tubing requires precise high-frequency ERW welding and post-weld seam planishing to ensure the seam does not split during tight-radius CNC mandrel bending.

  • Weight reduction of 20% to 30% per muffler core assembly.
  • High-yield strength ferritic stainless steel grades (409L, 439, 441).
  • Complete eddy-current seam testing post-perforation.
Technical Benchmarking

Material & Perforation Performance Comparison Matrix

Selecting the correct alloy chemistry and core geometry is essential for balancing acoustic attenuation, oxidation resistance, and unit production cost.

Alloy Grade / Core Type Max Temp (°C) Corrosion Resistance Thermal Expansion Primary Application Cost Index
409L (UNS S40900) 650°C - 700°C Moderate (Dry Exhaust) 11.5 × 10⁻⁶ /K Passenger Car Mufflers, OEM Tailpipes Economic
439 / 441 Ferritic 800°C - 850°C High (Condensate Resistant) 11.0 × 10⁻⁶ /K Hot-End Resonators, HEV Silencers Mid-Range
304 Austenitic 870°C Very High (Salt Spray & Acid) 17.2 × 10⁻⁶ /K High-Performance Exhaust, Marine Silencers Premium
316L Austenitic 920°C Superior (Chloride & Harsh Acid) 16.5 × 10⁻⁶ /K Heavy Duty Commercial & Marine Core Tubes Ultra-Premium
Aluminized Steel 500°C Basic (Short-Term Protection) 12.5 × 10⁻⁶ /K Budget Aftermarket Replacement Cores Entry Level
Manufacturing Excellence

Precision Manufacturing Process & Quality Control Engineering

VertexFlow operates an end-to-end vertically integrated production system in Foshan, China. Every step—from raw coil slitting to high-speed perforation, roll forming, continuous welding, and secondary CNC end-finishing—is monitored in real-time.

Step 1: Slitting & Surface Inspection

Precision slitting lines cut prime steel coils from TISCO, Baosteel, or POSCO into exact strip widths with zero edge burr, preventing edge misalignment during roll forming.

Step 2: High-Speed Rotary Perforation

Strips pass through custom high-speed rotary punch presses producing round holes (1.5mm to 6.0mm diameter) or louvered cutouts. In-line oil lubrication prevents punch heat buildup.

Step 3: Continuous ERW / TIG Welding

The perforated strip is roll-formed and seam-welded using TIG or High-Frequency Induction welding under inner argon gas shielding, preserving the stainless corrosion layer.

Step 4: Weld Seam Planishing & Sizing

Heavy hydraulic planishing rolls flatten the internal and external weld bead, ensuring smooth sliding during internal baffle assembly and packing insertion.

Step 5: CNC Cut-to-Length & End Forming

Automated cold saws cut core tubes to exact length tolerances (±0.2mm). Secondary rotary expanders flare or swage tube ends for quick slip-fit assembly.

Step 6: Ultrasonic Cleaning & Deburring

Finished core tubes undergo multi-stage ultrasonic degreasing to remove punching lubricants, followed by mechanical deburring to yield smooth, ready-to-pack components.

Compliance & Localization

Global Compliance Guarantees & Technical Support Network

VertexFlow ensures international OEM compliance across major global automotive markets including North America, the European Union, Japan, and Southeast Asia. We back every order with comprehensive chemical, mechanical, and dimensional certifications.

Certifications & Quality Traceability

Our facility operates under IATF 16949:2016 automotive certification and ISO 9001:2015 quality management systems. Every shipment includes EN 10204 3.1 Mill Test Certificates detailing raw coil heat numbers, chemical composition analysis, yield strength, elongation, and flattening test results.

Environmental & Material Safety

All products strictly adhere to EU REACH (EC 1907/2006) regulations, RoHS directives, and international Conflict Minerals reporting protocols. Our cleaning processes use closed-loop solvent recovery to minimize environmental impact.

Engineering Support & Rapid Prototyping

We provide complete OEM/ODM engineering collaboration. Send us your CAD drawings (STEP, IGES, DWG) or physical muffler core samples; our engineering team will return DFM (Design for Manufacturability) reports and custom prototype samples within 5 to 7 business days.

Precision Tubing Catalog Part II

Automotive Exhaust & Precision Structural Tubing

Explore our specialized automotive structural tubing, muffler core tubes, and special profile sections engineered for high-performance exhaust and industrial applications.
High-Quality Stainless Steel Tubing for Medical Safety Grab Bars Manufacturer, Supplier

High-Quality Stainless Steel Tubing for Medical Safety Grab Bars Manufacturer, Supplier

View Details
High-Quality Stainless Steel Handrail & Balustrade Tubing (ASTM A554) Manufacturers, Factory

High-Quality Stainless Steel Handrail & Balustrade Tubing (ASTM A554) Manufacturers, Factory

View Details
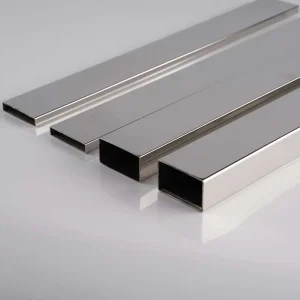
ODM ASTM A554 Stainless Steel Square & Rectangular Tubing Supplier, Factory

ODM ASTM A554 Stainless Steel Square & Rectangular Tubing Supplier, Factory

View Details
OEM Stainless Steel Tubing for Conveyor Rollers Manufacturers, Suppliers

OEM Stainless Steel Tubing for Conveyor Rollers Manufacturers, Suppliers

View Details
High-Quality ASTM A554 Stainless Steel Round Tubing (Ornamental & Structural) Manufacturer, Suppliers

High-Quality ASTM A554 Stainless Steel Round Tubing (Ornamental & Structural) Manufacturer, Suppliers

View Details
OEM Stainless Steel Tubing for Home Appliances & Electric Tools Factories, Factory

OEM Stainless Steel Tubing for Home Appliances & Electric Tools Factories, Factory

View Details
Wholesale Automotive Structural Tubing for Seats & Chassis Manufacturers, Manufacturer

Wholesale Automotive Structural Tubing for Seats & Chassis Manufacturers, Manufacturer

View Details
High-Quality Automotive Exhaust & Muffler Tubing (409L / 304) Suppliers, Factories

High-Quality Automotive Exhaust & Muffler Tubing (409L / 304) Suppliers, Factories

View Details
Buyer Knowledge Base

Frequently Asked Questions: Wholesale Muffler Core Tubes & Manufacturing

Technical answers curated by VertexFlow's metallurgical engineers and quality assurance directors to assist global procurement teams.
What stainless steel grades are best suited for automotive muffler core tubes?
For standard OEM automotive exhaust systems, 409L ferritic stainless steel is the industry standard due to its excellent combination of low thermal expansion, good thermal fatigue resistance, and cost efficiency. For hot-end resonators or environments subject to severe acid condensation (such as Hybrid Electric Vehicle cold-starts), Grade 439 or 441 stainless steel offers enhanced chromium and titanium stabilization. For high-performance tuning exhausts, marine mufflers, or extreme salt environments, Austenitic 304 or 316L stainless steel is specified for maximum corrosion resistance and aesthetic durability.
How does perforation pattern and hole pitch impact muffler acoustic performance?
The perforation pattern (staggered vs. straight inline) and open area ratio (OAR) directly control the acoustic impedance and backpressure of the muffler. Typically, an open area ratio between 20% and 32% provides the optimal balance for dissipative silencers, allowing sound waves to pass freely into the acoustic packing material without causing excessive exhaust gas turbulence. Smaller holes (e.g., 1.8mm to 2.5mm) effectively attenuate higher frequency sounds, while larger holes or louvered cutouts target lower frequency engine boom.
Can VertexFlow supply custom louvered core tubes instead of standard round perforated holes?
Yes. We manufacture both standard round-hole perforated core tubes and custom louvered core tubes. Louvers act as directional sound baffles that scoop sound waves into the fiberglass sound-dampening chamber while maintaining smooth linear gas flow along the center core. We possess over 500 tooling sets for various louver heights, angles, and pitches.
How do you ensure the weld seam does not split during secondary bending or expansion?
Weld seam cracking during CNC tube bending or end-expansion is usually caused by excessive weld bead hardening or incomplete weld penetration. VertexFlow utilizes high-frequency ERW or plasma-TIG welding with online continuous seam annealers and hydraulic weld planishing rollers. This process matches the weld ductility to the base parent metal. Every batch undergoes 100% flattening and flare expansion quality checks prior to shipment.
What secondary end-forming operations can be performed at your factory?
We provide full secondary manufacturing including CNC precise cut-to-length (deburred end), end expansion/swaging, end flaring, bead rolling, slotting, notch cutting, and lock-seam outer casing integration. Delivering assembly-ready core tubes eliminates double-handling and scrap costs for our OEM clients.
What is the minimum order quantity (MOQ) and production lead time for custom OEM core tubes?
Our standard Minimum Order Quantity (MOQ) is 500 kg per size for existing tooling profiles. For custom non-standard perforation patterns requiring new punch die creation, tooling lead time is 7 to 10 days, and full mass production lead time is typically 15 days from drawing approval. Fast-track prototype samples can be produced within 5 business days.
How are export shipments packaged to prevent transit damage and moisture oxidation?
Perforated core tubes are individually sleeved or bundled with anti-scratch plastic film, treated with volatile corrosion inhibitor (VCI) moisture protection, and packed into heavy-duty corrugated plastic boxes or IPPC-certified ISPM-15 wooden crates. Reinforced steel frames are available for heavy container shipments to prevent crushing during ocean transit.