Directly sourced mill-finished, bright annealed, mechanically polished, and electropolished sanitary tubes calibrated to rigorous concentricity and weld seam tolerances.
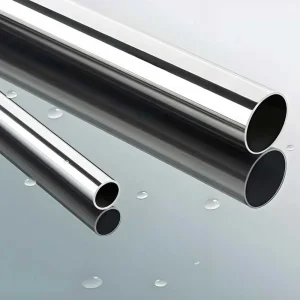
Engineered with structural 304/316 alloys, offering antimicrobial satin or mirror luster with extreme tensile yield.
Explore Specifications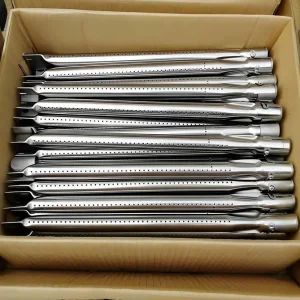
High-heat-resistant 304 and 409 grade precision punched and perforated gas tubes for continuous thermal cycling.
Explore Specifications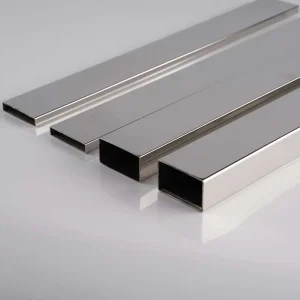
Precision-formed corners with straightness within 1mm/m and squareness within ±0.5° for architectural frameworks.
Explore Specifications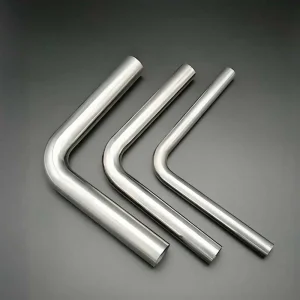
Flawless 600# mirror and hair-line satin finish tubes calibrated for tight-radius CNC rotary-draw bending.
Explore Specifications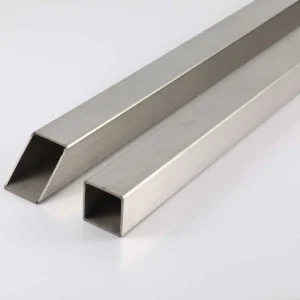
High-sanitation 304/316 tubes resisting aggressive medical disinfectants, hypochlorite solutions, and autoclaving.
Explore Specifications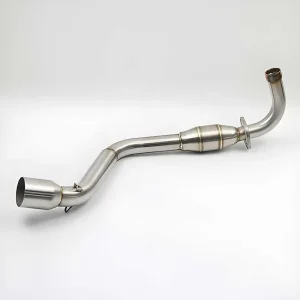
Formed for high vibration endurance, high thermal fatigue resistance, and tight expansion-swaging compliance.
Explore Specifications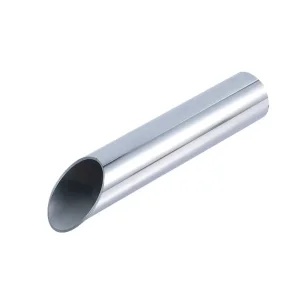
Solid cleanroom-ready 28mm lean-tubing replacing plastic-coated alternatives; zero particle shredding or peeling.
Explore Specifications
Molybdenum-enhanced (2.0–3.0% Mo) austenitic steel surpassing 500 hours neutral salt spray testing without pitting.
Explore SpecificationsNavigating evolving ASTM A270-S2, ASME BPE-2022, DIN 11866, and ISO 2037 mandates: Mitigating rouge, biofilm colonization, and orbital weld failure in mission-critical process loops.
Modern ultra-clean production in pharmaceutical WFI (Water for Injection) and aseptic food lines cannot tolerate surface anomalies. Conventional welded decorative tube exhibits micro-crevices and erratic ferrite boundaries that trap bacterial colonies (Pseudomonas, Listeria).
Our sanitary series undergoes longitudinal plasma-TIG fusion followed by automated planishing and inner electropolishing, maintaining a pristine chromium-to-iron oxide ratio (≥ 1.5) that permanently eliminates micro-fissures.
A primary bottleneck in biotech plant construction is automated orbital weld rejection due to pool deflection and erratic arc travel. This instability stems from inconsistent strip sulfur chemistry.
VertexFlow strictly refines heat runs to hold sulfur content precisely between 0.005% and 0.017% as specified by ASME BPE Part MM. This controlled Marangoni convection ensures repeatable weld bead geometry, total root fusion, and zero concavity without manual burn-through.
Regulatory scrutiny from the FDA, EMA, and global hygiene inspectors requires full material lineage. Every batch of VertexFlow sanitary tube is marked with indelible laser serialization tracking back to the original ladle refining furnace.
Shipped lots include complete EN 10204 Type 3.1 Mill Test Reports encompassing chemical composition, flattening resistance, tensile yield, elongation, eddy-current scan logs, and borescopic optical roughness profiles.
Engineered across austenitic 304, 304L, 316L (UNS S31603), and high-molybdenum 1.4435 (Basel Standard) formulations. Standardized to worldwide pharmacopeia tolerances.
| Standard / Designation | Material Grade | Inner ID Finish (Ra Metric) | Outer OD Polish | Weld Planishing & Annealing | Primary Industrial Field |
|---|---|---|---|---|---|
| ASME BPE SF1 | AISI 316L / 1.4404 | Ra ≤ 0.51 μm (20 μin) Mech Polish | 180 / 240 Grit (Ra ≤ 0.8 μm) | Fully Beaten Weld, Bright Annealed | Biotech / Clean Steam |
| ASME BPE SF4 | 316L / Low Ferrite (<1%) | Ra ≤ 0.38 μm (15 μin) Electropolish | 320 Grit / 600# Mirror | Vacuum Degreased, 1050°C H2 Anneal | WFI / Vaccine Bulk API |
| DIN 11866 Series B | 1.4435 (Mo ≥ 2.7%) | Ra ≤ 0.25 μm (10 μin) Electro Chem | Satin 240# Longitudinal | Continuous In-Line Eddy-Current Monitored | European Sterile Pharma |
| 3-A Standard 33-03 | AISI 304 / 304L | Ra ≤ 0.80 μm (32 μin) Mech Clean | 180 Grit Sanitary Satin | Inner Weld Bead Removed, Level with Wall | Dairy, Beverage, CIP Loops |
| ISO 2037 / BS 4825 | 304L / 316L | Ra ≤ 0.80 μm to 1.0 μin | Bright Annealed (Unpolished OD) | Cold Drawn / Roll Formed Plasma Fused | Brewery & Food Grade Lines |
In high-purity biopharmaceutical operations, delta ferrite can convert to sigma phase under prolonged thermal exposure, inducing micro-cracking and rouge. Our sanitary 316L grades are formulated to maintain a magnetic ferrite content below 1.0% (FN < 2) for maximum corrosion resistance in hot WFI lines.
Mechanical polishing leaves microscopic directional tears and plastically deformed cold-worked layers. Our electrochemical polishing process electro-dissolves high-energy micro-peaks, producing an amorphous, super-smooth chromium-enriched passive layer that drops contact angle and resists protein binding.
Every single length of VertexFlow sanitary tubing is subjected to non-destructive testing (NDT) according to ASTM A1016. In addition to in-line electromagnetic eddy-current checking, pipe sections endure 100% hydrostatic pressure testing up to 250 bar (dependent on wall gauge) without weeping.
From single-cell fermentation suites to high-speed dairy processing plants, our sanitary pipe infrastructure underpins global critical utilities.
Use Cases: Bioreactor harvesting loops, WFI distribution manifolds, pure steam generation, chromatographic purification skids.
System Benefits: Extreme tolerance conformity (OD ±0.05 mm) ensures frictionless orbital autogenous welding. Ultra-low carbon profiles avoid intergranular sensitization during autoclave cycles and steam cleaning at 135°C.
Use Cases: High-temperature short-time (HTST) pasteurizers, milk gathering skids, aseptic filling carousels, automated Clean-In-Place (CIP) / Steam-In-Place (SIP) systems.
System Benefits: Compliance with 3-A 33-03 and EHEDG standards guarantees that caustic soda (NaOH) and nitric acid wash cycles rinse clean with zero chemical retention or flavor cross-contamination.
Use Cases: Specialty gas bulk pipelines (nitrogen, argon, silane), cleanroom deionized water plants, etching agent transport lines.
System Benefits: Vacuum baked and nitrogen-sealed with moisture contamination down below parts-per-billion (ppb) thresholds. Particle count testing conforms to Class 1 cleanroom assembly standards.
Driving manufacturing excellence through low-carbon melting routes, in-line nanometer laser profilometry, and smart laser serialization.
VertexFlow is transitioning annealing thermal units to 100% green hydrogen atmospheres. This eliminates carbon footprint in the heating cycle while dramatically lowering surface carbon pickup, yielding an exceptionally stable, scale-free, uncarburized passive chromium oxide matrix.
Every millimeter of tube internal bore is scanned using 360-degree rotary optical interferometers. Real-time machine learning algorithms detect microscopic weld undercut, inclusions, or variations exceeding 0.05 μm instantly, quarantining anomalies before final cutting.
In response to international nickel and molybdenum volatility, our engineering lab is qualifying advanced duplex (2205) and low-nickel austenitic compositions that maintain PREN ≥ 35 while resisting localized stress-corrosion cracking in high-chloride marine and spa installations.
Supplying multinational EPC contractors, pharmaceutical skids builders, and sanitary distributors across North America, Europe, the Middle East, and Southeast Asia.
Each pipe is individually capped with clean PE closures, encased in high-density polyethylene heat-sealed sleeves, and bundled in vapor-corrosion-inhibitor (VCI) barrier materials to prevent marine salt contamination in transit.
Reinforced fumigated wooden cases lined with heavy corrugated polymer shielding ensure zero deformation, scratching, or bending deflection during crane handling and ocean container freight.
We provide comprehensive CO (Certificate of Origin), Form E, RCEP documentation, and customs compliance advice, helping distributors optimize clearance costs into the US, European Union, and ASEAN zones.
Our bilingual metallurgy engineers support remote factory acceptance testing (FAT), material validation checklists, third-party SGS/TÜV inspector coordination, and quick turnaround custom profile tooling.
Authoritative metallurgical and practical engineering answers addressing ASME BPE compliance, surface Ra measurements, and welding performance.
Meeting commercial, structural, and precision engineering procurement requirements with rigorous mill standards.
Ultra-smooth plating substrate tubing with Ra ≤ 0.4 μm and completely eradicated inner weld witness lines.
Explore Specifications
High structural load-bearing stainless rails preventing hanger deflection, pitting, or chrome peeling in humid spaces.
Explore Specifications
Nitrogen-shielded welded tubes in 201/304/316 alloys, featuring high tensile strength and deep draw bendability.
Explore Specifications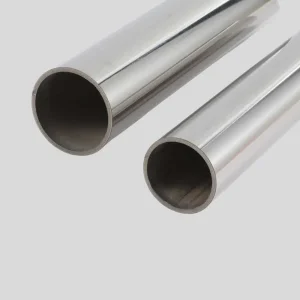
Engineered with minimal Total Indicator Runout and strict 1mm/m straightness for high-speed automated sorting.
Explore Specifications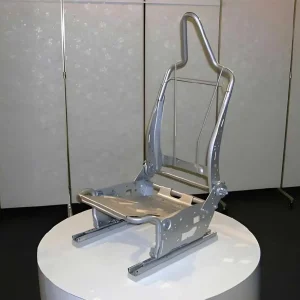
High-yield crash-resistant stainless profiles engineered to strict automotive OEM tolerances and cyclic loading.
Explore Specifications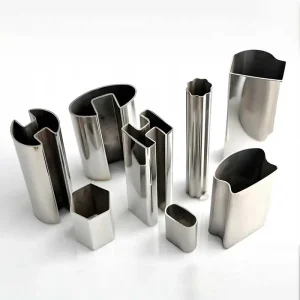
Utilizing over 500 existing forming roll dies to deliver flat-oval and D-shaped profiles without tooling fees.
Explore Specifications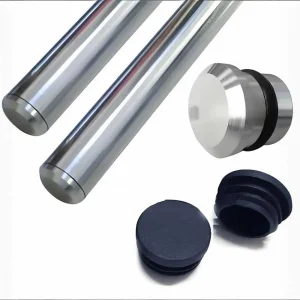
Precision-formed 304 components for water heaters, heat exchangers, handles, and electrical motor casings.
Explore Specifications
High-definition satin and mirror balustrade tubing with tight end-face deburring for seamless field welding.
Explore SpecificationsNeed strict ASME BPE SF4 electropolishing verification, custom wall thicknesses, tight bend radii calculations, or EN 10204 3.1 certification packs? Our Foshan technical team provides comprehensive engineering reviews within 24 hours.